Precision brazing and heat treating for critical metal parts

Brazing, heat treating and nitriding for OEMs and Tier 1 suppliers since 1943 — from prototype to high-volume production.

Scroll down

Eastlake and Cleveland, Ohio

Vacuum, furnace and induction brazing — and the heat treating that goes with it

Over 100 metal services across our Northeast Ohio plants. Send the drawing and the spec, and our quote team takes it from there.

Send us your parts.
Or order the braze aids we make.

01.

Contract services

Brazing, heat treating and nitriding to your print and spec

  • Nadcap accredited brazing and heat treating at HiTech Aero
  • Furnace brazing in accordance with AMS
  • Vacuum, hydrogen, argon, nitrogen, helium and exothermic atmospheres
  • Prototype, short-run and high-volume production

Braze aids

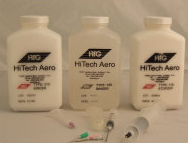
Stop offs and binders, made by HTG

  • Type 110 Stop Off and Type 215 Binder
  • Formulated for vacuum and controlled atmosphere furnaces
  • Clean up with warm detergent and water
  • Sold in one-quart containers
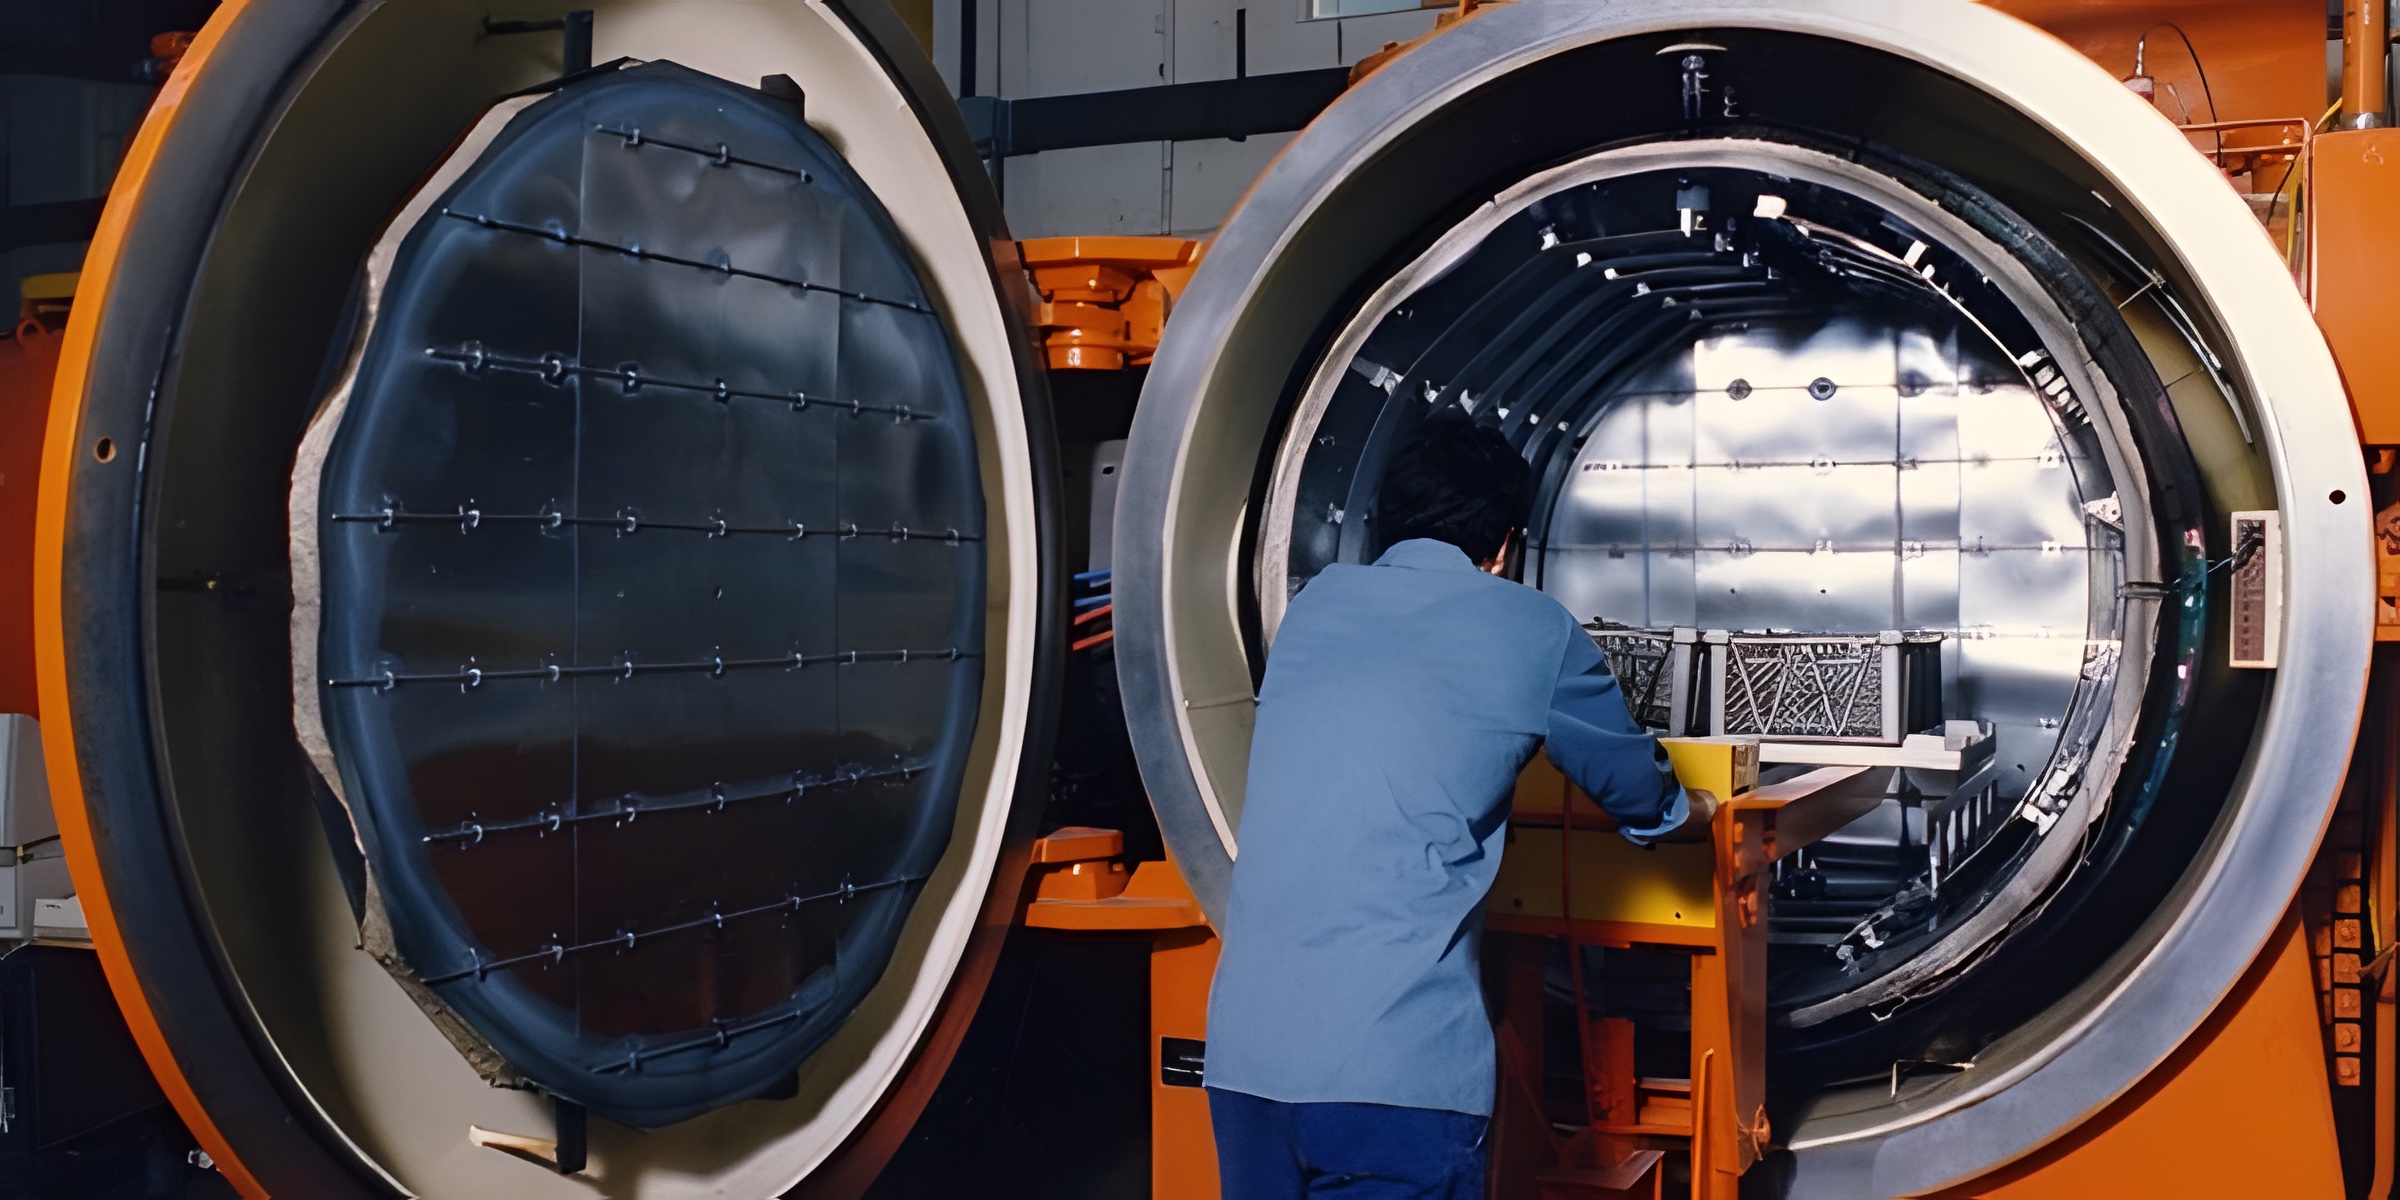
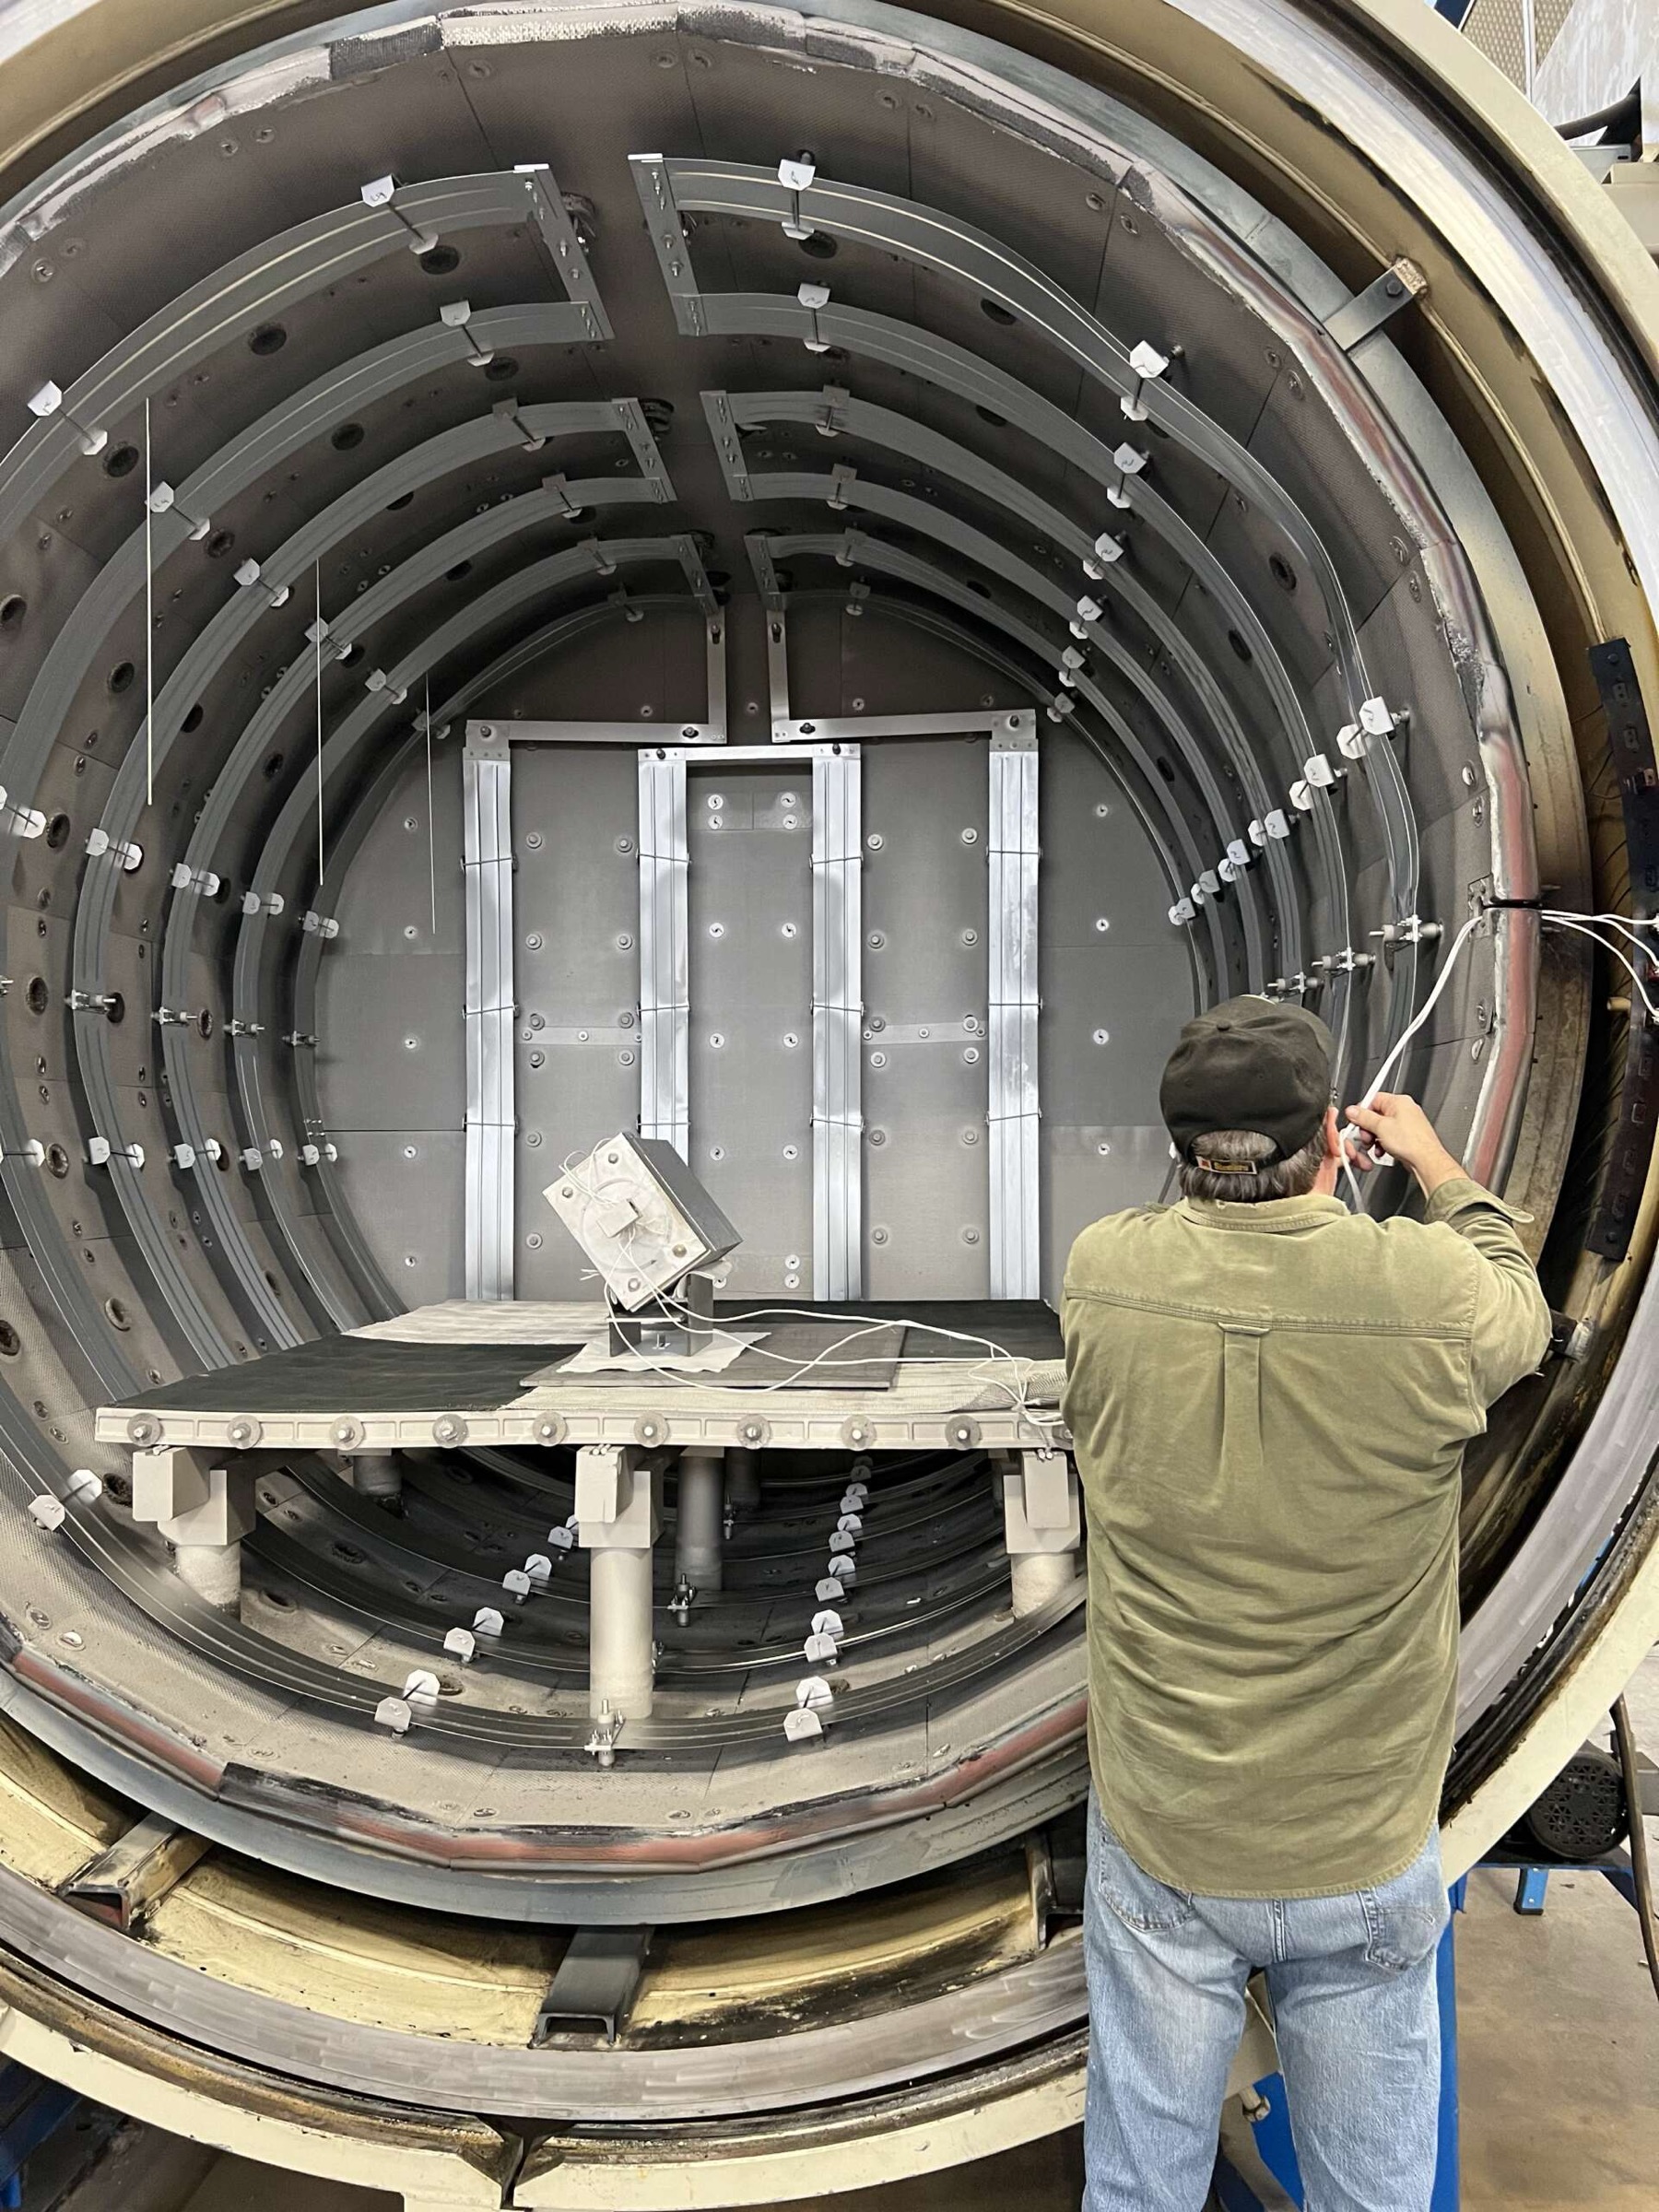
Operator loading a vacuum furnace at Walker Heat Treat, Cleveland

Have a part that needs brazing or heat treating?

Tell us the material, the spec and the quantity — the quote team takes it from there.

Request a quote

Industries we work for

Aerospace, automotive, fluid power and hydraulics, food processing, transportation, tooling and die casting, military and industrial manufacturing — from critical aircraft components to high-volume automotive parts.

See our processes
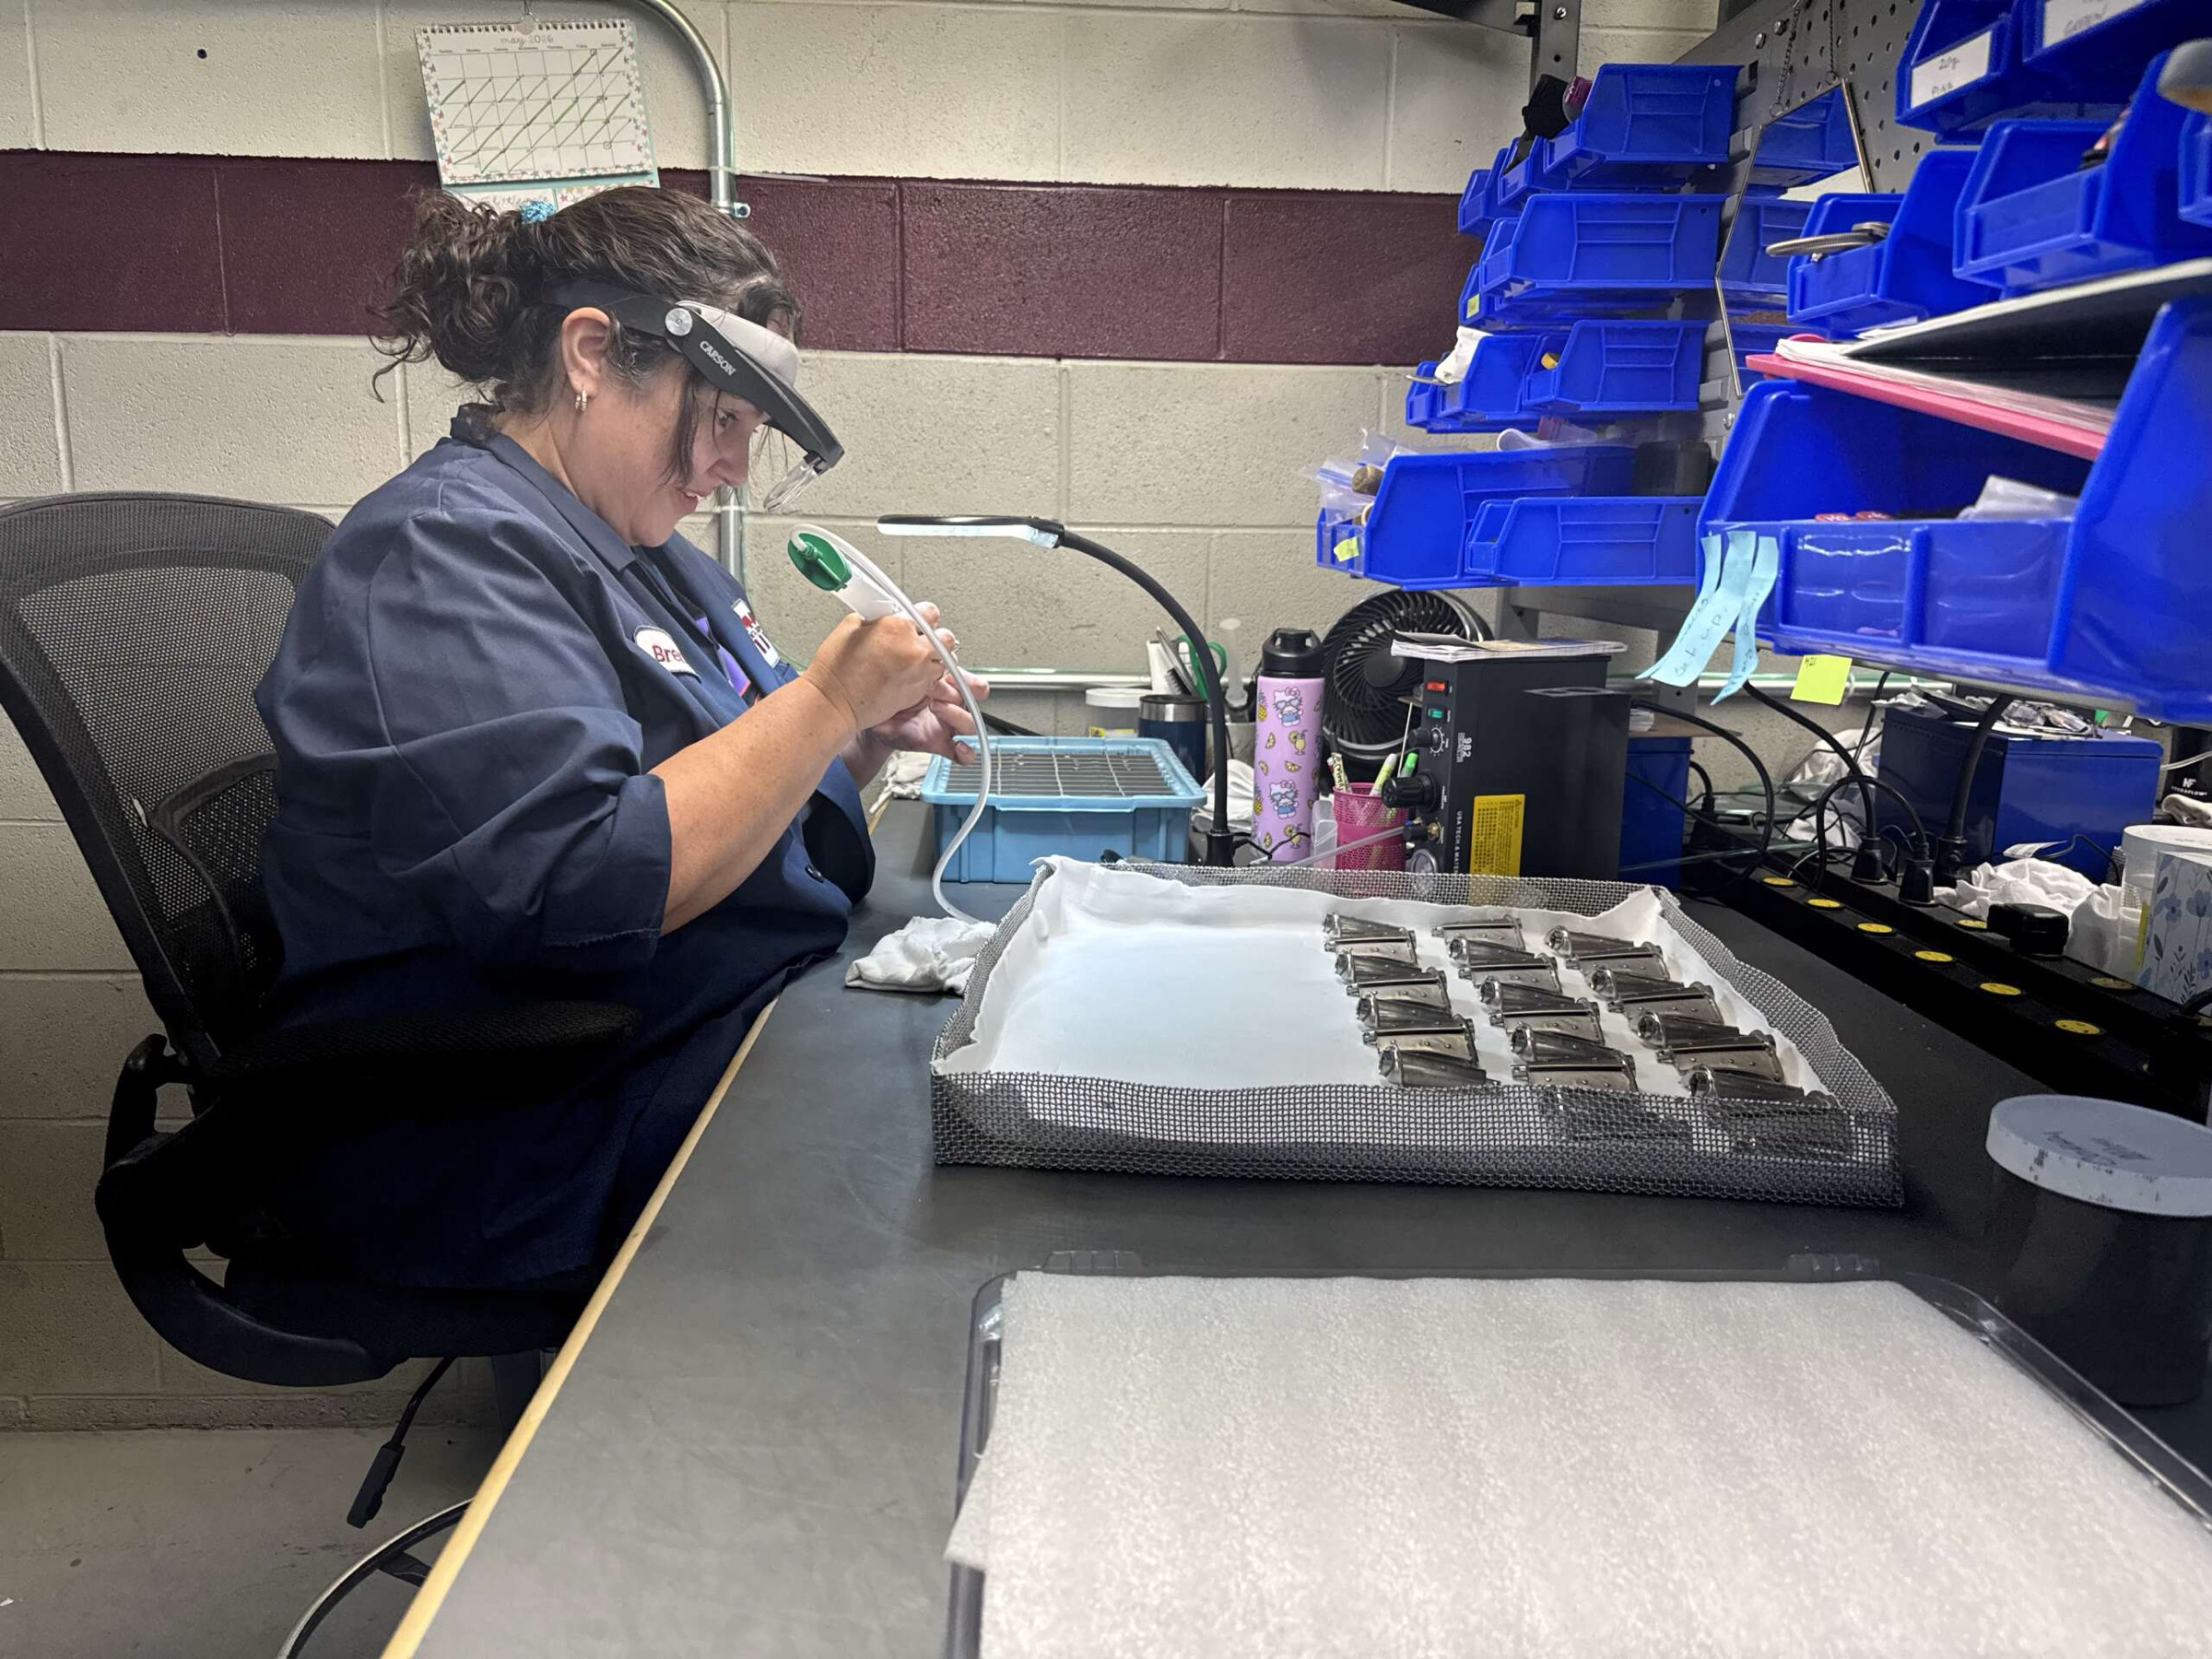
An HTG inspector checking brazed parts at the bench

About HTG

HTG started in 1943 as Technical Metal Processing. Today our plants braze, heat treat and nitride parts for aerospace, hydraulics, automotive and food equipment builders — working directly with OEMs and Tier 1 suppliers.

HiTech Aero

Eastlake, Ohio. Nadcap accredited heat treating and brazing, AS9100D with ISO 9001:2015. Vacuum furnaces up to 60″ × 72″, a hydrogen continuous belt furnace and a hydrogen retort.

Walker Heat Treat

Cleveland, Ohio. Tool steel specialists since 1946, part of HTG since 1986. 24-hour service on many tool steel treatments.

“Right Today, Better Tomorrow.”

Ourcoreprocesses

1.

Brazing

Furnace, vacuum, induction and torch brazing in protective atmospheres — exothermic, pure dry hydrogen, argon, nitrogen, helium or vacuum — for bright, clean, well-wetted joints. We braze stainless and carbon steels, nickel alloys such as Monel 400, Inconel 600 and Hastelloy, OFHC copper, beryllium copper and lead-free brass, with gold, silver, copper and nickel filler metals.
  • In accordance with AMS
  • Nadcap at HiTech Aero
  • Fluxless vacuum brazing
  • Step brazing
  • Titanium and tantalum
An HTG technician working inside an open vacuum brazing furnace
2.

Heat treating

Annealing, hardening, normalizing, stress relieving, quench and temper, and age and precipitation hardening — in atmosphere, induction and vacuum furnaces. Cryogenic treatment goes as low as −300 °F. Heat treating relieves stress in fabricated parts and sets their strength, ductility and hardness.

  • Vacuum up to 60″ × 72″
  • Hydrogen belt furnace
  • Cryogenic to −300 °F
  • Tool steel at Walker

−300°F

Cryogenic treatment, at the cold end of our range. Vacuum furnaces at HiTech Aero run up to 60″ × 72″.

3.

Brazing engineering

Joint design, material selection, proof of concept and design for manufacturability. Our engineers pick the right process for your base metals — continuous furnace, vacuum or induction — review rejected brazements to find the cause, and set what to inspect after brazing.

  • Joint design
  • Design for manufacturability
  • Failure review
  • Cost reduction
4.

Nitriding and
NITRIDETEK FNC

Gas nitriding of ferrous alloys at low temperatures, for lower distortion and tight control of case thickness. NITRIDETEK ferritic nitrocarburizing adds a hard, wear-resistant surface and a black finish with corrosion resistance comparable to medium grades of stainless steel.

  • Gas and vacuum nitriding
  • Ferritic nitrocarburizing
  • Parts up to 3,000 lb and 48″ long

700–1200°F

Gas nitriding range. Lower processing temperatures mean lower distortion.

Request a quote

Over 100 metal services in all. Not sure which process fits? Ask the quote team.

Brazed assemblies

Made to your print, from prototype and short runs to high-volume production.

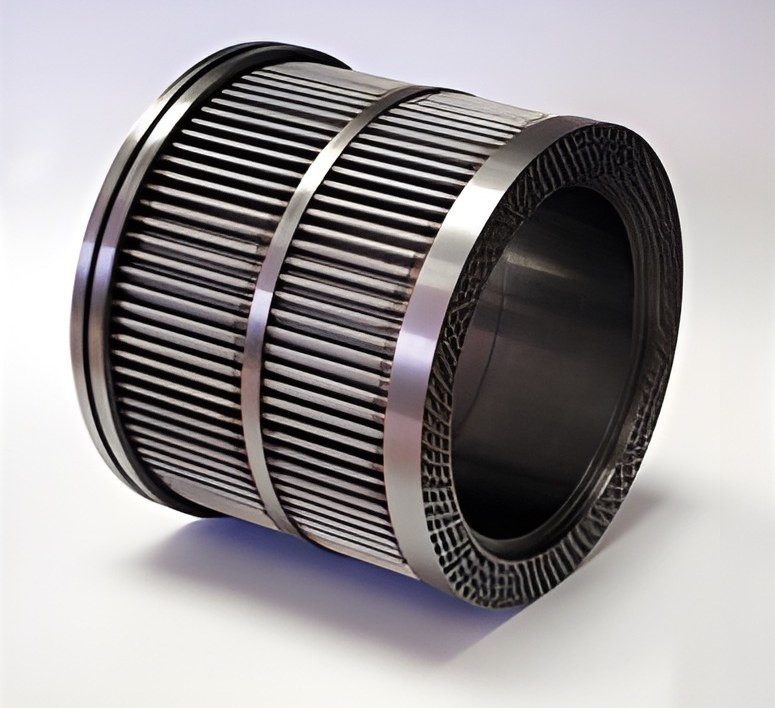
Hydraulic manifolds
  • Stacked lamination
  • Prototype to production

Hydraulic manifolds

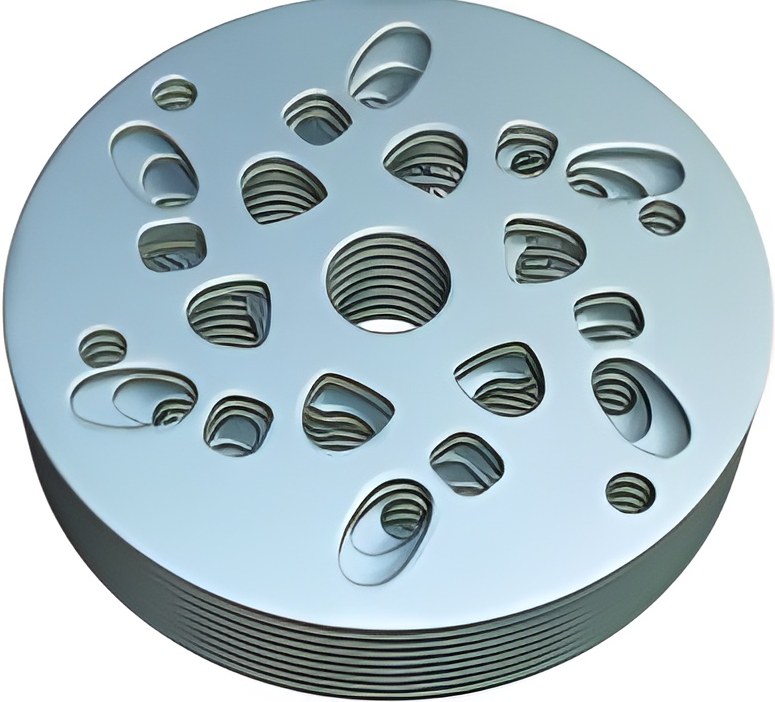
Stamped steel plates stacked and brazed into one manifold. Small, precise fluid channels with no cross-drilled passages to plug.

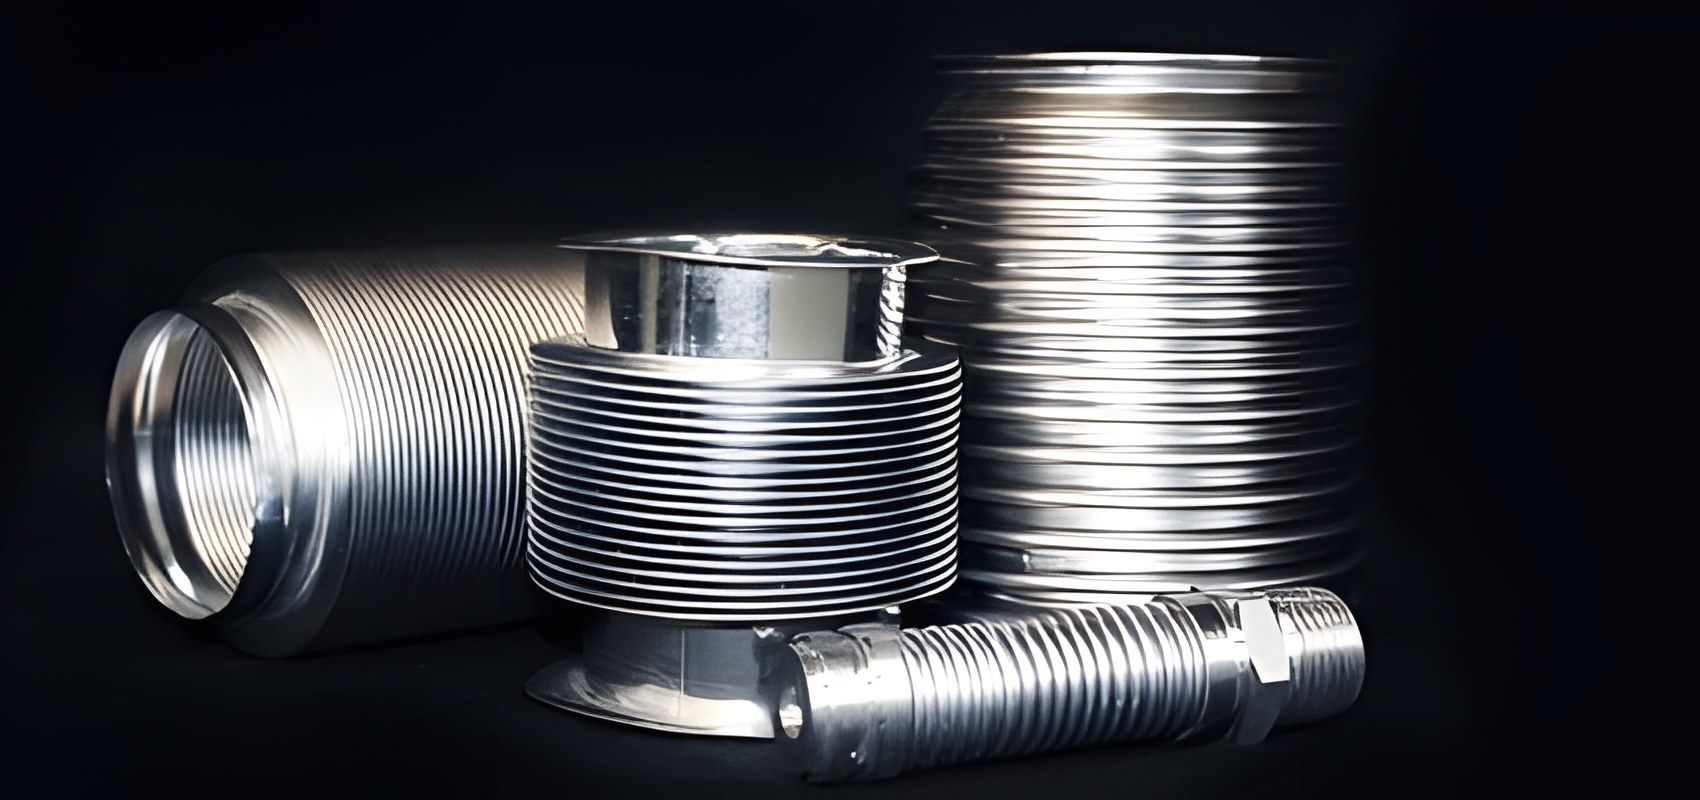
Bellows assemblies
  • 1/4" to 4" OD
  • Custom ends

Bellows assemblies

Brazed metal bellows in beryllium copper, brass, stainless steel and Monel, made from closed-end seamless tube.

Heat exchangers
  • Tube and shell
  • Plate and frame

Heat exchangers

Brazed tube and shell, plate and frame, and brazed plate heat exchangers for oil coolers, heat pumps and marine use.

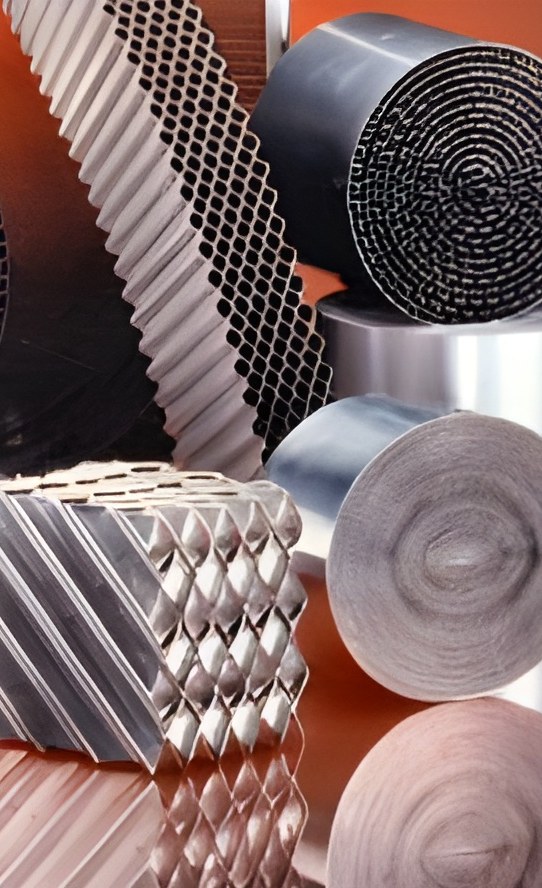
Honeycomb and metallic substrates
  • 50–600 CPSI
  • Since the early 1980s

Honeycomb and metallic substrates

HTG began forming metallic honeycomb for jet engines in the early 1980s. Today: corrugated and honeycomb substrates in custom shapes and cell sizes.

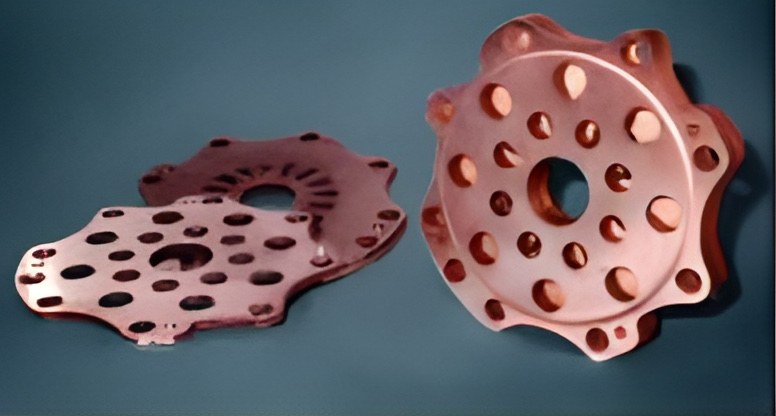
Brazed laminated assemblies
  • Copper and steel
  • Close tolerance

Brazed laminated assemblies

Stacked stamped components held in fixed relation and brazed together, for close-tolerance internal features.

Braze aids made by HTG

Sold in one-quart containers.

HTG braze aid quarts: Type 215 Binder (left) and Type 110 Stop Off (right)Type 110 Stop Off
  • Vacuum
  • Controlled atmosphere
  • 1 qt

Type 110 Stop Off

Stays put. Will not run. Requires no stirring.

Keeps braze filler out of threads, holes and narrow tubes, and keeps stacked parts from bonding to each other or to fixtures.

Apply by brush, roller, squeeze bottle or pneumatic dispenser. Can be automated with metered flow.

HTG braze aid quarts: Type 215 Binder (left) and Type 110 Stop Off (right)Type 215 Binder
  • Vacuum
  • Controlled atmosphere
  • 1 qt

Type 215 Binder

A suspension medium for powdered filler metals.

Burns cleanly and leaves little residue, so joints are clean and easy to inspect. Contains no lacquer base.

Apply by brush, dip, roll or automatic applicator.

Request a quote

Upload the drawing, pick the process and spec, and tell us how many. That's what the quote team needs to price the job.

Headquarters and sales

34800 Lakeland Blvd.
Eastlake, OH 44095

(216) 881-8100quoteteam@htg.cc

HiTech Aero

34800 Lakeland Blvd., Eastlake, OH
(216) 426-6850

Walker Heat Treat

10601 Briggs Rd, Cleveland, OH 44111
(216) 941-0440

Tell us about the part

01 The work
02 Spec and quantity
03 Drawing or spec sheet

Drop your drawing here

PDF, STEP, DWG, DXF or images, up to 8 files

04 Your details

Certifications